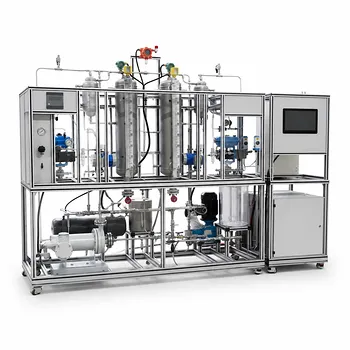
A two-stage series membrane configuration transforms a hydrogen recovery pilot plant from a simple demonstration into a sophisticated tool for studying industrial optimization. The immediate benefit is the ability to combine high hydrogen recovery (over 90%) with reduced recompression energy. The first membrane unit captures a large fraction of hydrogen at an elevated pressure, while the second unit scavenges the remaining hydrogen from the retentate, ensuring maximum yield without sacrificing the permeate pressure that makes downstream compression affordable.
A single membrane stage forces a hard compromise between recovery and permeate pressure. Staging two units in series breaks that compromise, letting researchers precisely map the trade-off between hydrogen yield, operating pressure, and energy consumption—exactly the knowledge needed to design efficient industrial gas recovery systems.
The Challenge of Single-Stage Membrane Separation
A single membrane unit faces an unavoidable physical constraint that directly impacts economics.
The Inherent Conflict Between Recovery and Permeate Pressure
Hydrogen permeation is driven by a partial pressure difference. To push recovery to a high fraction, you must let the retentate’s hydrogen concentration drop significantly. But doing so lowers the permeate-side pressure toward the end of the membrane, because less driving force remains available. That low-pressure permeate is expensive to recompress for reuse.
Conversely, if you maintain a high permeate pressure to save on compression, you must stop recovery earlier and leave more hydrogen behind in the retentate. You simply cannot maximize both variables at the same time with a single pass.
Why a Compromise isn’t Enough for High-Purity Hydrogen Streams
In applications like ammonia plant purge gas—where hydrogen content can exceed 60%—the economic stakes are high. Recompressing large volumes of low-pressure permeate can erase the savings from recovering the hydrogen. Yet leaving significant amounts of hydrogen in the waste stream is a direct yield penalty. The pilot plant must therefore recreate the conditions that teach engineers to navigate this energy-versus-recovery dilemma.
How a Two-Stage Series Design Solves the Conflict
Placing two membrane units in series decouples the recovery process into two distinct pressure regimes.
Stage One: High-Pressure Permeate for Low-Cost Recompression
The first membrane unit operates exactly like the “compromise” stage you would avoid. It recovers a large portion of the hydrogen at a high permeate pressure. Because the retentate still holds a fair amount of hydrogen, the partial pressure differential remains strong, and the permeate emerges at a pressure that minimizes the compression work needed to return it to the process.
Stage Two: Deep Recovery of Residual Hydrogen
The retentate from Stage One—now enriched in inert gases but still containing valuable hydrogen—enters the second membrane unit. This second stage is deliberately operated to pull the hydrogen fraction down to very low levels. It produces a permeate at a lower pressure, but the volume of this low-pressure stream is now much smaller. The bulk of the hydrogen was already recovered efficiently in Stage One.
The Result: Over 90% Recovery with Better Energy Management
The combined system can exceed 90% hydrogen recovery while the majority of the permeate is captured at high pressure. The pilot plant becomes a platform to vary the split between stages, membrane area, and operating pressures, revealing exactly how recovery yield, permeate pressure, and compressor energy consumption interact under realistic industrial conditions.
Understanding the Trade-offs
The two-stage design is not universally perfect. Its value depends entirely on what you need to learn or achieve.
Increased Capital and Operational Complexity
A second membrane housing, associated pipework, and extra instrumentation introduce additional capital cost and maintenance points. For a pilot plant focused purely on simple hydrogen separation, a single stage can be sufficient. The series design only justifies itself when the goal is to quantify the energy–recovery trade-off, not just to produce hydrogen.
The Diminishing Returns of Additional Stages
While a two-stage setup dramatically improves the recovery–pressure balance, adding a third stage usually delivers marginal gains. The retentate after two stages is already lean in hydrogen, so the incremental recovery requires a large membrane area for a small stream at near-vacuum permeate pressure. The pilot plant setup with exactly two stages is a sweet spot for demonstrating meaningful process optimization without needless complexity.
Matching Pilot Plant Goals to Design
If the pilot plant is intended for educational or research purposes, the two-stage configuration is a superior teaching tool. It forces users to confront the design choices that real plants face: how much compression cost is acceptable, and at what point does additional recovery become uneconomical? A single stage hides these dynamics behind a single setpoint.
The Pilot Plant as a Teaching Tool for Process Optimization
Beyond the specific membrane hardware, the two-stage system visualizes broader chemical engineering principles.
Demonstrating Inert Rejection and Yield Penalty Reduction
Many processes—hydrotreating, hydrogenation, ammonia synthesis—suffer from inert gas buildup that lowers reactant partial pressure. The pilot plant shows how directing these high-pressure purge gases through a staged membrane recovers hydrogen while rejecting inerts like methane. It directly validates the concept of reducing yield penalties and increasing reactor throughput without changing the core reactor.
A Platform for Experimenting with Real-World Operational Parameters
With independent control over each membrane stage’s pressures and flow paths, researchers can systematically map the response surface of recovery vs. energy. This moves the learning beyond theory and into practical, measured trade-offs that mirror what engineers face when retrofitting hydrogen recovery onto existing plants.
Making the Right Choice for Your Pilot Plant Goals
- If your primary focus is maximizing recovery yield above all else: A two-stage series configuration is essential. You’ll reach >90% hydrogen recovery while still collecting most of it at a pressure that keeps recompression feasible.
- If your primary focus is minimizing pilot plant complexity and capital cost: A single membrane stage suffices. You’ll still demonstrate separation but at the expense of a realistic energy–recovery trade-off study.
- If your primary focus is education on industrial gas recovery optimization: The two-stage setup is the definitive choice. It exposes the exact decision-making process engineers use to balance permeate pressure, compression energy, and product loss.
In the end, the two-stage series membrane configuration turns a simple separation experiment into a compact, high-fidelity model of real-world hydrogen recovery economics.
Summary Table:
| Feature / Metric | Single-Stage Configuration | Two-Stage Series Configuration |
|---|---|---|
| Hydrogen Recovery | Moderate (compromised to maintain pressure) | High (exceeds 90% yield) |
| Permeate Pressure | Low (if high recovery is targeted) | High for bulk stage; low only for scavenge stage |
| Recompression Energy | High (large volume of low-pressure gas) | Low (majority of gas recovered at high pressure) |
| System Complexity | Low (single housing, basic instrumentation) | Higher (dual housing, advanced control valves) |
| Research/Educational Value | Limited (simple demonstration tool) | High (ideal for mapping energy-recovery trade-offs) |
Elevate Process Education and Research with LABPARK
To bridge the gap between classroom theory and industrial reality, academic and research labs need equipment that models complex process economics. LABPARK provides state-of-the-art Educational and Vocational Unit Operations Pilot Plants in chemical engineering, bioprocess & biotech, and environmental & water treatment for universities, research institutes, and enterprises.
Our custom-engineered pilot systems—including multi-stage membrane separation plants—allow researchers and students to experiment with real-world variables like pressure differentials, energy recovery, and system optimization.
Ready to upgrade your laboratory or training facility? Contact LABPARK today to explore our customizable pilot plant solutions and request a technical consultation.
Related Products
- Alkaline Membrane Water Electrolysis Educational Pilot Plant Unit Operations Training System
- Multifunctional Membrane Separation Educational Pilot Plant with Ultrafiltration, Nanofiltration, Reverse Osmosis
- Multi-Functional Membrane Separation Educational Pilot Plant for Unit Operations Lab
- Ultrafiltration Membrane Separation Educational Pilot Plant
- Multi Functional Membrane Crystallization Educational Unit Operations Pilot Plant
People Also Ask
- How do chemical engineering pilot plants demonstrate electrolysis? Bridge Theory & Industrial Scale
- How do alkaline and PEM electrolysis technologies differ in pilot plant operations?
- Why is the selection of electrode materials critical when configuring or operating educational electrolysis pilot plants?
- Bipolar vs Monopolar Electrolysis: Key Configuration Details to Analyze in Pilot Plants
- Which Electrolysis Pilot Plant Parameters Ensure Safety & Efficiency? Key Controls Explained