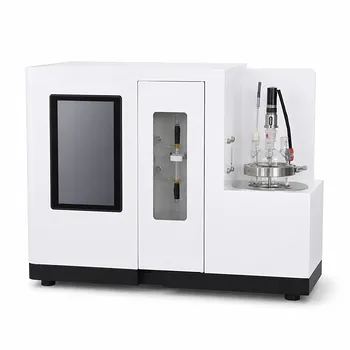
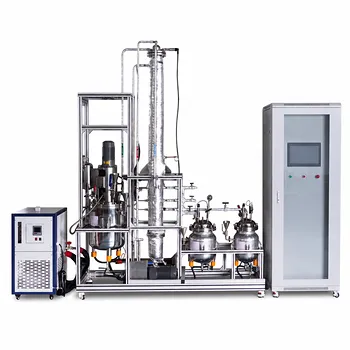
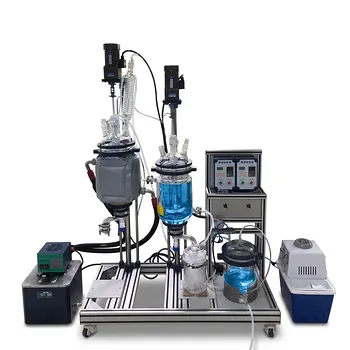
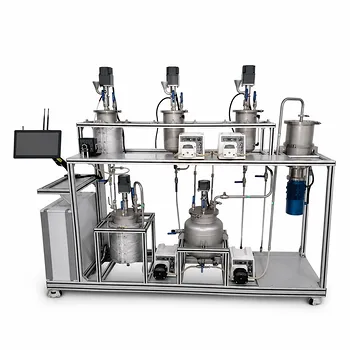
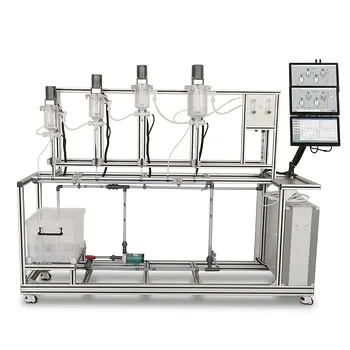
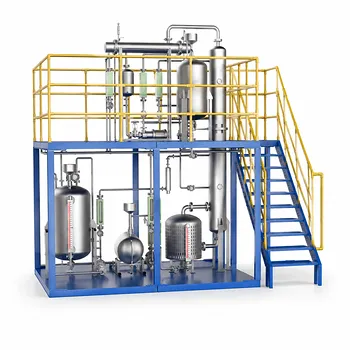
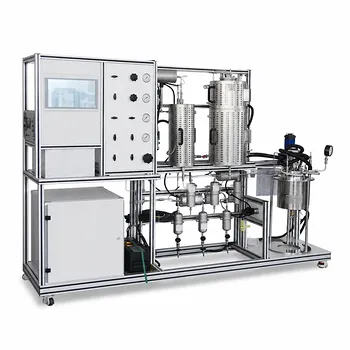
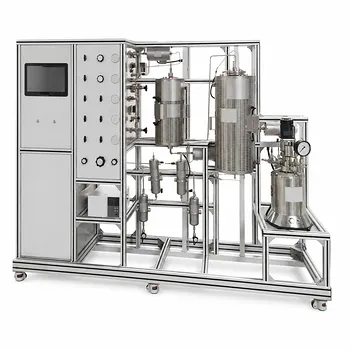
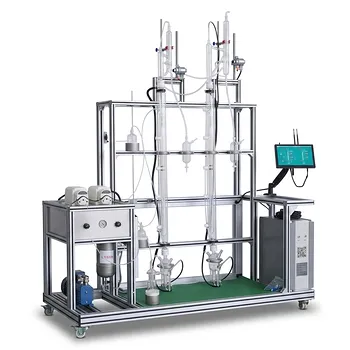
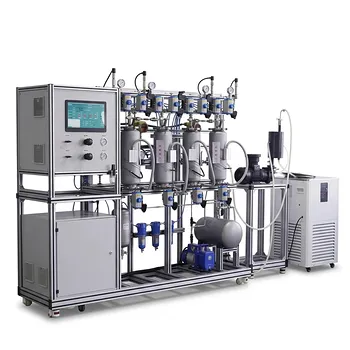
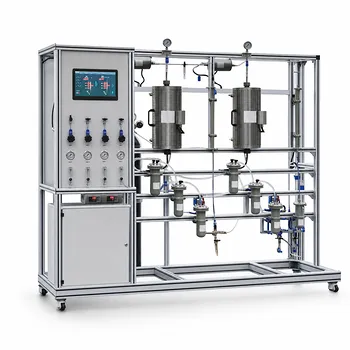
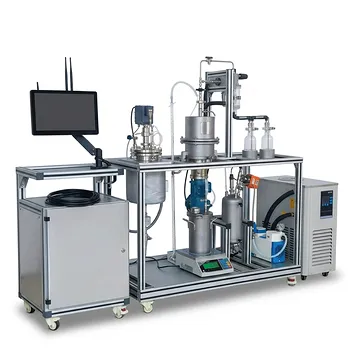
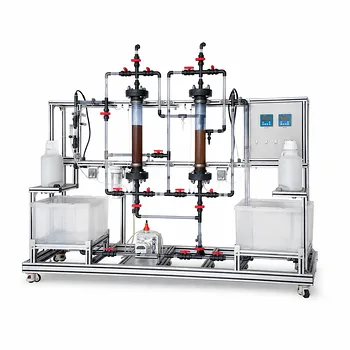
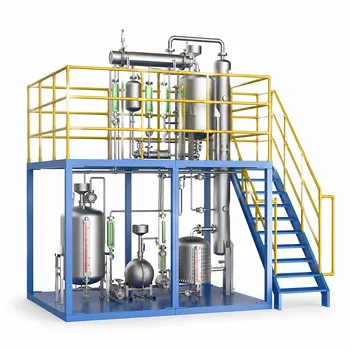
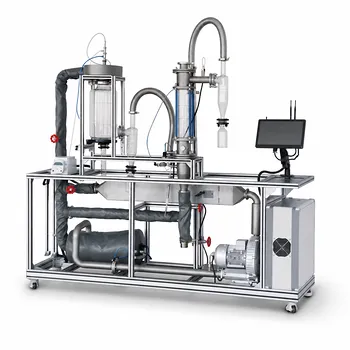
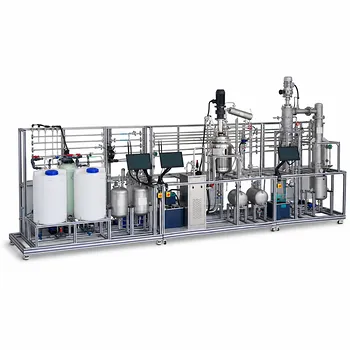
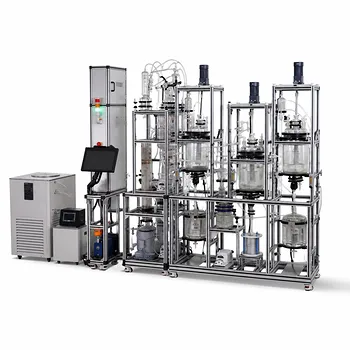
The MSMPR crystallizer pilot plant directly answers a fundamental chemical engineering challenge: how to make population balance equations tangible. It provides an idealized, well-mixed environment where the crystal size distribution (CSD) inside the vessel perfectly matches the product stream. By measuring that CSD at steady state, students can plot the data and extract key kinetic parameters—nucleation rate and crystal growth rate—using a simple straight-line model. This bridges the gap between differential equations on a whiteboard and the reality of a flowing, crystallizing process.
The real value lies not in just measuring crystal sizes, but in allowing students to see the population balance as a predictive tool. An MSMPR pilot plant turns abstract theory into a hands-on experiment that reveals how operating choices (residence time, feed rate, stirring speed) directly shape the final crystal size distribution.
The MSMPR Concept: Why Uniform Mixing Matters
The acronym MSMPR (Mixed Suspension, Mixed Product Removal) is a design promise. The pilot plant is engineered to maintain a perfectly uniform suspension and an identical composition in both the vessel and its discharge stream. This idealized state is the key to educational simplicity.
An Idealized Laboratory for Kinetic Measurement
Without this uniformity, modeling crystal size distribution becomes a computational nightmare. Real tanks often have zones of varying temperature, supersaturation, and particle concentration. The MSMPR design eliminates those gradients. Students can therefore assume a single set of conditions throughout the vessel, making the math tractable and the results directly interpretable.
The Steady-State Assumption as a Learning Tool
The pilot plant is operated until it reaches a steady state, where the continuous feed and removal stabilize. At that point, the incoming mass equals the outgoing mass, and the crystal population inside the vessel remains constant. This steady-state condition removes the time variable from the population balance, turning a partial differential equation into a simple algebraic relationship that can be tested on a benchtop.
From Raw Data to Kinetic Insight: Applying the Population Balance
Once steady state is reached, the pilot plant’s true pedagogical power emerges. Measuring the CSD is just the beginning; the real lesson comes from applying the population balance equation to that data.
The Straight-Line Equation That Unlocks Kinetics
For an ideal MSMPR crystallizer, the steady-state population balance reduces to a linear form:
ln n = ln n⁰ – L/(G τ)
Here, n is the population density (number of crystals per unit size per unit volume), L is the crystal size, G is the linear growth rate, and τ is the residence time (volume divided by volumetric flow rate). Students take their CSD data, calculate n for each size fraction, and plot ln n versus L.
Calculating Growth and Nucleation Rates
The resulting plot yields a straight line whose slope is –1/(G τ). Since the residence time τ is a known operating parameter, the crystal growth rate G is solved directly. The intercept of that line, ln n⁰, gives the nuclei population density, and from that the nucleation rate B⁰ = n⁰ G is calculated. Suddenly, two critical crystallization parameters—nucleation and growth—are no longer abstract; they are numbers derived from a student’s own experimental work.
Connecting the Math to the Product
These calculated kinetic parameters then become the bridge to understanding product quality. A faster nucleation rate relative to growth will produce many small crystals (a fine, narrow CSD), while slower nucleation and faster growth yield a small number of larger crystals. By varying the residence time τ or stirrer speed, students can directly observe how these kinetic responses shift the final size distribution, cementing the link between process and outcome.
Hands-On Learning: How the Pilot Plant Bridges Theory and Practice
An MSMPR unit does more than just generate data; it forces students to confront the messy reality of process control while still providing a structured learning environment.
Exploring the Metastable Zone Visually
Industrial crystallization is often operated in the metastable zone—the region between the solubility curve and the point where spontaneous primary nucleation explodes. The pilot plant allows precise control of cooling rates and stirrer speeds. Students can deliberately manipulate these variables to keep the solution’s supersaturation within this zone, visually seeing how controlled growth produces larger, more uniform crystals. Stray outside that zone, and the CSD immediately reflects an unwanted burst of fine nuclei. This is a powerful demonstration of process stability that no textbook can replicate.
Bridging Mass Balances and Unit Operations
In a curriculum that often separates reaction engineering from transport phenomena, the MSMPR crystallizer acts as a unifying case study. It combines a material balance (the population of crystals) with an energy balance (cooling) and mass transfer (nucleation and growth). Running the pilot plant teaches students to simultaneously consider thermodynamics, kinetics, and fluid dynamics—exactly the skill set required for designing and troubleshooting real unit operations.
Understanding the Trade-offs and Limitations of the MSMPR Model
The educational value is greatest when students also learn what the model cannot do. An MSMPR pilot plant is an idealization, and recognizing its limitations builds true engineering judgment.
When Real Crystallizers Deviate from Ideal Mixing
The model assumes perfect mixing and size-independent growth. In reality, crystals can settle, agglomerate, or break. A student observing a curved, rather than straight, line on the ln n vs. L plot learns that these non-idealities are present. This teaches them to question assumptions and to use the model as a diagnostic tool, not a perfect oracle. The deviation itself becomes a learning point about fluid mechanics and particle interactions.
The Challenge of Steady-State Patience
Achieving true steady state can take many residence times, requiring patience and rigorous sampling protocols. This practical constraint teaches the discipline of experimental design: taking samples too early yields misleading kinetics. Educators must plan for this operational reality, using the waiting time to reinforce the mathematics behind the approach to steady state.
Making the Most of an MSMPR Pilot Plant in Education
To extract the full pedagogical value, the plant must be used as more than a data-collection device. Here’s how to align your lab objectives with the right learning outcome.
- If your primary focus is understanding nucleation theory: Use the intercept (n⁰) to calculate the nucleation rate and compare it to classical nucleation models. Challenge students to explain why nuclei population density changes with mixing speed.
- If your primary focus is kinetic parameter estimation: Run the system at multiple residence times (by changing feed flow rates) and observe how the CSD shifts. Verify that growth rate G remains consistent, then map out nucleation vs. supersaturation curves.
- If your primary focus is process optimization: Have students operate within the metastable zone and then deliberately crash the system into uncontrolled nucleation. Let them design a cooling profile that maximizes mean size while minimizing fines—turning theory into a quantitative design challenge.
The MSMPR crystallizer pilot plant remains an unparalleled bridge: it converts a set of differential balances into a vision of a growing crystal population that students can touch, measure, and control.
Summary Table:
| Parameter / Variable | Symbol | Educational & Practical Significance |
|---|---|---|
| Population Density | $n$ | Represents crystal quantity per size fraction; plotted as $\ln n$ vs. $L$. |
| Crystal Size | $L$ | The independent variable; used to analyze size distribution deviations. |
| Growth Rate | $G$ | Solved directly from the slope of the steady-state plot ($-1 / G\tau$). |
| Residence Time | $\tau$ | Volumetric flow control parameter used to manipulate final crystal size. |
| Nucleation Rate | $B^0$ | Calculated as $n^0 G$; shows the rate of new crystal formation. |
Bring Industrial Crystallization to Your Chemical Engineering Lab
Equip your students and researchers with hands-on learning solutions that turn abstract math into tangible process insights. LABPARK provides premium Educational and Vocational Unit Operations Pilot Plants in chemical engineering, bioprocess & biotech, and environmental & water treatment. Designed specifically for universities, research institutes, and enterprises, our pilot plants bridge the gap between classroom theory and industrial reality.
Ready to upgrade your engineering curriculum? Contact LABPARK today to explore our custom pilot plant solutions!
Related Products
- Multi Functional Membrane Crystallization Educational Unit Operations Pilot Plant
- Carbon Material Thermal Pretreatment Multiphase Separation Educational Pilot Plant
- Potassium Salt Thermal Dissolution and Crystallization Separation Educational Unit Operations Pilot Plant
- High-Gravity Emulsification and Mass Transfer Educational Pilot Plant
- Multi-Stage Stirred Tanks in Series Residence Time Distribution and Mixing Performance Determination Educational Pilot Plant
People Also Ask
- Why is precise temperature control critical in crystallization pilot plants? Key to Scale-Up Success
- Control Crystallization Pilot Plant Secondary Nucleation: 4 Key Adjustments
- What key factors should be considered when configuring a crystallization unit operations pilot plant?
- What are the benefits of integrating online PAT tools like ATR-FTIR into crystallization unit operations pilot plants?
- How to use crystallization pilot plant agitation speed to identify diffusion vs reaction growth?