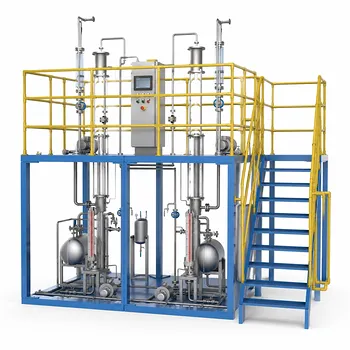
Sparger design dictates bubble size and distribution, which directly controls gas holdup—but only when you’re operating in the right flow regime. In a multiphase bubble column pilot plant, using a single-nozzle sparger produces significantly lower gas holdup than multinozzle or porous plate designs at low gas velocities. As you push into the slug flow regime at higher superficial gas velocities, however, the sparger’s influence fades, and gas holdup becomes nearly independent of the disperser geometry.
The sparger governs gas holdup primarily in the bubbly flow regime by determining the number and size of bubbles formed. Once the system transitions to slug flow, hydrodynamics take over and the initial bubble size matters far less. For pilot-scale studies, the practical takeaway is that sparger choice is most critical when working at low gas velocities, where you’re likely characterizing mass transfer performance or validating reactor models.
The Regime-Dependent Behavior of Spargers
Low Gas Velocity: Where Sparger Choice Rules
At low superficial gas velocities, the liquid phase remains relatively undisturbed, and bubbles rise individually. The sparger determines the initial bubble population. A single orifice creates larger, fewer bubbles that rise quickly, giving less gas holdup. Multinozzle or sintered plate spargers, by contrast, inject gas through many fine openings, creating a swarm of smaller bubbles that linger longer and increase the volume fraction of gas in the column.
This regime is where educational pilot plants and characterization studies spend most of their time. The primary reference confirms that the distinction is vital for demonstrating gas-liquid mass transfer principles. Students measuring holdup with different spargers can directly observe how bubble size distribution alters residence time and interfacial area.
When Slug Flow Takes Over
As gas velocity increases, bubbles coalesce and form large slugs that span the column diameter. The flow structure becomes controlled by the column geometry and the buoyancy of the slugs, not by the initial bubble size produced at the sparger. In this regime—highlighted by the primary reference—the effect of sparger design on gas holdup becomes insignificant.
The practical implication is that if your pilot plant operates mainly in the churn-turbulent or slug regime to mimic industrial reactors, you can simplify your sparger selection. However, if you plan to run across a wide range of velocities for kinetic studies, you must account for the transition and avoid misinterpreting data taken in the sparger-sensitive region.
How Sparger Type Dictates Bubble Dynamics and Holdup
Single-Nozzle vs. Multinozzle vs. Porous Plates
A single-nozzle sparger generates the simplest gas distribution, but also the lowest holdup. The larger bubbles it produces have a shorter residence time and present a smaller total gas-liquid interfacial area. Multinozzle crosses improve distribution by splitting the gas stream into multiple smaller jets, increasing the number of bubbles and therefore holdup, though coalescence can still occur a short distance above the distributor.
Porous plates and sintered metal diffusors produce the finest primary bubbles. The supplementary references confirm that these designs yield higher mass transfer coefficients, with a parameter b reaching 1.174–1.445 for sintered plates versus only 0.460–0.467 for nozzle crosses. This tripling or quadrupling of the volumetric mass transfer coefficient is a direct consequence of the higher gas holdup and interfacial area they create.
Sintered Plates and Mass Transfer Intensification
Beyond holdup itself, the choice of sparger drives the volumetric liquid-side mass transfer coefficient (k_L a). The supplementary references note that sintered plates and two-phase nozzles can increase k_L a by a factor of 4 to 5 compared to standard spargers. For a pilot plant used in education or process intensification research, switching sparger types becomes a keystone variable—one that teaches the link between bubble mechanics and reactor efficiency.
Because gas holdup and k_L a are tightly coupled, the sparger’s impact on holdup translates directly into differences in reaction rate and conversion. This makes sparger design a primary lever for optimizing performance in gas-liquid reactions where mass transfer is the limiting step.
Ensuring Pilot Plant Data is Representative
Column Diameter and Internals – What Doesn’t Change
When scaling up from a pilot plant, you need to know what factors remain constant. For columns larger than 0.15 meters in diameter, gas holdup becomes virtually independent of column width, pressure up to 1.6 MPa, and even the presence of internals like draft tubes or multistage distributors. This means that data collected on a properly sized pilot column can be scaled with confidence, provided you’ve chosen a sparger that matches the intended industrial distribution profile.
The supplementary references also stress that standard single-stage bubble column correlations remain reliable for columns with internals. So if your pilot plant includes internal heat exchangers or baffles, you don’t need to worry about these features distorting the sparger’s baseline influence on holdup.
Liquid Properties and Their Interplay
The sparger’s effect does not act in isolation. Liquid viscosity, density, and surface tension co-determine bubble size and coalescence behavior. High-viscosity liquids suppress bubble breakage, leading to larger bubbles and lower gas holdup irrespective of sparger type. When using a pilot plant for education, students can vary liquid properties and observe how a sparger that performs well in water may yield very different holdup in a viscous organic solution.
Ionic strength also plays a subtle role. The supplementary references introduce an ionic strength factor f that modifies holdup correlations. Coalescing media like pure water allow bubbles to merge rapidly after formation, which can mute the initial advantage of a fine-pore sparger. In such systems, the sparger’s influence may be partially overridden unless bubble coalescence is inhibited.
Understanding the Trade-offs
Choosing a high-performance sparger like a sintered plate is not without downsides. These spargers can clog if solids are present, require higher pressure drop to operate, and may be difficult to clean. For pilot plants handling slurries or sticky materials, a robust multinozzle cross may provide more reliable operation while still offering adequate holdup for characterization.
Another pitfall lies in misapplying data from the sparger-sensitive flow regime. If you collect holdup data at low gas velocities with a finely porous sparger and then attempt to predict performance for an industrial reactor that operates in the churn-turbulent regime with a simple pipe sparger, your extrapolation will be flawed. The primary reference’s emphasis on the slug flow regime warns against this oversimplification.
Finally, backmixing is an inherent disadvantage of sparged bubble columns, especially as gas holdup increases. A sparger that maximizes holdup can exacerbate liquid-phase backmixing, which may reduce reaction selectivity. Pilot plant designers must balance the desire for high interfacial area against the risk of non-ideal flow patterns that distort kinetic measurements.
Making the Right Choice for Your Pilot Plant Goal
Your selection of sparger type should directly support the purpose of your pilot plant study. Use the following criteria to guide your decision.
- If your primary focus is educational demonstrations of mass transfer: Use a sintered plate or two-phase nozzle to accentuate the effect of bubble size on holdup and k_L a. This creates a stark contrast with a simple single-nozzle and reinforces core chemical engineering principles.
- If your primary focus is generating scalable data for reactor design: Choose a sparger that mimics the expected industrial distributor. Operate in a column larger than 0.15 m diameter and keep gas velocities within the regime where holdup is sparger-independent to ensure your correlations transfer.
- If your primary focus is maximizing mass transfer in a clean, low-viscosity system: Deploy a porous plate sparger to achieve up to a 5‑fold increase in k_L a, but account for potential coalescence if you switch to non-coalescing media.
- If your primary focus is handling solids or fouling feedstocks: Prioritize reliability over peak holdup. A multinozzle cross with large orifices will resist plugging and still provide acceptable gas dispersion in the transitional flow regime.
A sparger is never just a gas inlet—it’s a tool for shaping the hydrodynamic environment of your pilot plant. Match it to your operating regime and your study’s objective, and you’ll turn gas holdup into a controlled variable rather than a source of confusion.
Summary Table:
Sparger Performance Comparison in Bubble Column Pilot Plants
| Sparger Type | Bubble Size | Gas Holdup | Best Suited For |
|---|---|---|---|
| Single-Nozzle | Large | Low | Fouling feeds, slurry handling, and simple hydrodynamics |
| Multinozzle Cross | Medium | Moderate | Industrial scale-up modeling and robust routine operations |
| Porous / Sintered Plate | Fine / Small | Very High | Educational mass transfer demos & process intensification |
Optimize Your Process Engineering & Training with LABPARK
Understanding gas-liquid hydrodynamics is essential for accurate research and impactful training. LABPARK provides premium Educational and Vocational Unit Operations Pilot Plants in chemical engineering, bioprocess & biotech, and environmental & water treatment for universities, research institutes, and enterprises.
Our custom-engineered pilot systems help you:
- Enhance Education: Visually and quantitatively demonstrate flow regimes, bubble mechanics, and mass transfer principles.
- Ensure Scalable Research: Generate reliable, representative data to confidently scale up multiphase reactor processes.
- Customize Configurations: Easily test diverse sparger designs, internals, and liquid properties on a single platform.
Equip your facility with the tools to bridge the gap between theory and industry. Contact LABPARK today to discuss your pilot plant requirements!
Related Products
People Also Ask
- How do two-film & penetration theories apply to gas absorption pilot plant teaching? Key pedagogical insights.
- How does partial pressure behavior influence gas absorption pilot plants? Master Mass Transfer
- How is the direction and driving force of mass transfer determined in a gas absorption unit operations pilot plant?
- Why does increasing flow fail to enhance absorption in fast chemical reactions? Pilot Plant Insights
- What are the limitations of Henry's Law in gas absorption pilot plants? Avoid critical lab errors.