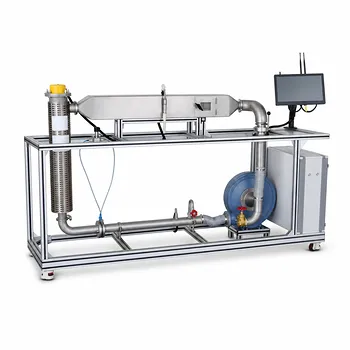
The answer starts with a measurement. To determine the overall heat transfer coefficient (K) for a shell-and-tube heat exchanger in a pilot plant, you run the unit under steady-state conditions, measure the inlet and outlet temperatures and mass flow rates of both fluids, and calculate the actual heat duty (Q). Using the known heat transfer area (A) and the log mean temperature difference (\Delta T_m), you then solve (K = Q/(A \cdot \Delta T_m)). This experimental value is your most accurate figure for that specific setup—but it comes with strict boundaries.
Core Takeaway
Experimental measurement gives a (K) value that is unquestionably accurate for your pilot plant’s current fluid, fouling state, and geometry. But its real power lies in what it teaches you about the design trade‑off: a lower (K) forces a larger, costlier exchanger, while a higher (K) shrinks the unit but demands more aggressive (and expensive) operation. Choosing where to sit on that curve is the central engineering decision.
The Experimental Backbone: Measuring K Directly
Steady-State Data Collection
The only way to get a trustworthy overall coefficient is to capture data when the plant is thermally stable. That means all temperatures and flow rates must hold constant for a sufficient period.
In a shell‑and‑tube pilot plant, you measure the four terminal temperatures (hot in/out, cold in/out) and the mass flow rates of both fluids. Without steady operation, the heat balance won’t close and your (K) will be meaningless.
The Heat Duty and LMTD Calculation
Once you have stable data, you calculate the actual heat transferred. Use the heat balance on whichever fluid gives the more reliable measurement: (Q = \dot{m} c_p \Delta T).
Next, determine the true driving force. For a single‑pass shell‑and‑tube exchanger, the log mean temperature difference (LMTD) is non‑negotiable, especially when temperature approaches are close. The counter‑current LMTD is standard, corrected if the flow arrangement is multi‑pass.
Solving for the Overall Coefficient
With (Q), the exchanger’s known outer tube area (A_o), and the LMTD, (K_o) (based on the outer surface) becomes a simple division. This single number encapsulates all the thermal resistances—film coefficients, wall conduction, and current fouling layers—without needing to measure them individually.
The Role of Empirical Correlations and Verification
Typical Ranges for Cross-Checking
Every pilot‑plant measurement should face a sanity check. Standard industrial reference ranges serve this purpose perfectly.
For a clean water‑to‑water exchanger, expect (K) to fall between 850 and 1700 W/(m²·°C). For water with condensing steam, typical values soar to 1420–4250 W/(m²·°C). If your experimental number sits wildly outside these brackets, suspect an instrumentation error or severe fouling.
When to Trust Empirical Values
Empirical ranges are not a substitute for measurement—they are a training tool and a starting point for early‑stage design. In a pilot‑plant context, they let you verify student calculations quickly and provide a conservative base when historical data is absent. They never capture the specific thermal penalty of your unit’s particular scale buildup, fluid velocity profile, or baffle arrangement.
Design Implications: How Your K Value Shapes the Pilot Plant
The Capital vs. Operating Cost Trade-Off
The choice of (K) is fundamentally an economic lever. Selecting a lower design (K) forces the exchanger to grow in surface area; the equipment gets heavier, occupies more plot space, and costs more upfront.
However, that same conservative selection often reduces long‑term operating strain—you can achieve the required duty with smaller temperature driving forces or lower flow velocities. Conversely, a higher design (K) produces a compact, low‑capital unit but demands high turbulence, larger pumping power, and more frequent cleaning to maintain that performance. The pilot plant is your laboratory for mapping this trade-off before it becomes a full‑scale financial decision.
Dealing with Temperature-Dependent Properties
Many pilot‑plant fluids undergo substantial viscosity or thermal conductivity changes across the exchanger. When this happens, treating (K) as a constant distorts your calculated area badly.
If the variation is mild and nearly linear with temperature, you can use a modified heat‑rate equation that considers the local (K) at each end of the exchanger. If the change is strongly non‑linear, segment the exchanger into multiple sections where (K) can be assumed constant inside each slice, then integrate numerically. Ignoring this simply teaches the wrong lesson about scale‑up.
From Pilot Data to Scale-Up Decisions
An experimental (K) is valid only for the exact geometry, fluid pair, velocity field, and fouling condition you tested. When you scale up, similarity breaks down—the shell‑side cross‑flow velocity, baffle cut, and tube pitch ratio all shift the film coefficients.
Never transport a pilot‑plant (K) directly into a production design. Instead, use the pilot data to validate your predictive methods (like the shell‑side (j_h) correlations) and then apply those methods to the large‑scale geometry with proper fouling allowances.
Understanding the Trade-offs
The Specificity Trap of Experimental Data
A precisely measured (K) creates a false sense of security. If you unknowingly took data immediately after a cleaning cycle, your number boasts an unrepresentative high performance. If you failed to record the exact baffle spacing, that number cannot be related to future modifications. Experimental accuracy is narrow—it shines a bright light on a single point but leaves the surrounding map dark.
The Danger of Ignoring Fouling
Even in a pilot plant, fouling builds up. An overall coefficient measured today includes an unknown fouling resistance. Designing solely on a clean (K) leads to an undersized production exchanger that fouls to failure within weeks. Every design derived from pilot data must include an explicit, defendable fouling factor unless you are measuring the fouled coefficient directly over long‑term operation.
Balancing Accuracy with Simplicity
Decomposing (K) into individual film coefficients via the thermal‑resistance equation is academically powerful: it shows students exactly how tube diameter, wall conductivity, and velocity influence performance. Yet, collecting the separate measurements required for a full Wilson‑plot‑style analysis demands significant extra instrumentation. For many pilot‑plant objectives, the direct overall measurement—strengthened by a comparison to empirical ranges—strikes the best balance between insight and practical effort.
Making the Right Choice for Your Goal
- If your primary focus is education and hands‑on learning: Measure (K) experimentally under multiple flow rates, then compare your results against the established empirical ranges to build intuition.
- If your primary focus is scaling up to a production unit: Use the pilot plant to validate your film‑coefficient correlations (like the (j_h) method) and apply those to the full‑scale geometry with a conservative fouling allowance—never transplant the raw (K) directly.
- If your primary focus is optimizing an existing pilot‑plant exchanger: Map (K) as a function of shell‑side and tube‑side velocity to find the point of diminishing returns where higher pumping costs no longer justify the gain in heat transfer.
- If your primary focus is a quick, safe early‑stage design: Select a (K) from the low end of the empirical range for your fluid pair. This yields a larger, more forgiving surface area that protects against unknowns until pilot data can refine the number.
Every overall heat transfer coefficient you extract from a pilot plant is a snapshot of a specific set of resistances; use it wisely as a calibration point for your design judgement, not as a universal constant.
Summary Table:
| Aspect | Details | Design Implication |
|---|---|---|
| Measurement | Solve $K = Q / (A \cdot \Delta T_m)$ at steady state | Represents actual fouling and geometric conditions. |
| Empirical Range | Water-Water: 850–1700 W/(m²·°C) Steam-Water: 1420–4250 W/(m²·°C) |
Acts as a sanity check for sensor errors or heavy fouling. |
| Lower Design K | Requires larger heat transfer area | Increases initial capital cost but lowers operating strain. |
| Higher Design K | Requires high fluid velocity and turbulence | Reduces footprint but increases pumping power and fouling risk. |
| Scale-Up Rule | Validate local film correlations ($j_h$) first | Never copy pilot $K$ directly; scale up using verified correlations. |
Optimize Your Engineering Labs with LABPARK Pilot Plants
Accurately calculating heat transfer coefficients and understanding scale-up economics requires robust, reliable equipment. LABPARK offers premium Educational and Vocational Unit Operations Pilot Plants across chemical engineering, bioprocess & biotech, and environmental & water treatment.
We help universities, research institutes, and enterprises bridge the gap between academic theory and industrial practice with high-precision, safely designed pilot systems.
Ready to upgrade your laboratory capabilities? Contact LABPARK today to request a quote or custom design consultation!
Related Products
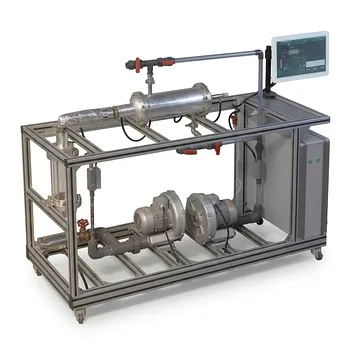
- Shell and Tube Heat Exchanger Heat Transfer Coefficient Determination Educational Pilot Plant
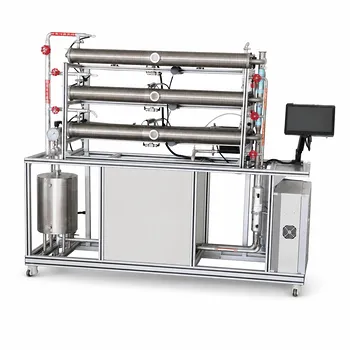
- Three-Tube Heat Transfer Educational Pilot Plant for Unit Operations Training
- Comprehensive Multi-Modal Heat Transfer Unit Operations Pilot Plant for Engineering Training
- Dual Mode Heat Transfer Pilot Plant for Unit Operations Training
- Circulating Wind Tunnel Drying and Convective Heat Transfer Coefficient Determination Educational Pilot Plant
People Also Ask
- Why Apply LMTD Correction in Shell-and-Tube Pilot Plants & How to Determine It
- How is the fouling factor (Rd) evaluated? Key Pilot Plant Insights for Students
- How is fouling factor demonstrated using shell and tube pilot plants? Practical Lab Guide
- Why is simulating and calculating fouling factors crucial when operating educational heat exchanger pilot plants?
- How do tube pitches affect equivalent shell diameter (De)? Math & pilot plant impact explained.