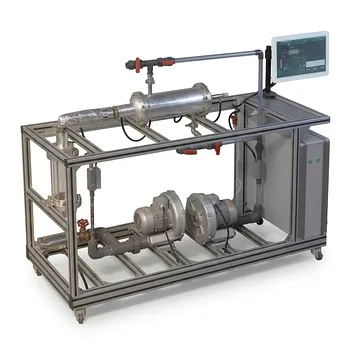
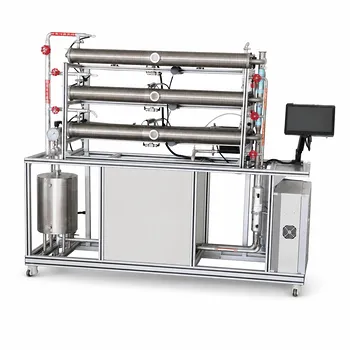
The choice of tube pitch geometry directly changes the equivalent shell-side diameter (De) and cross‑sectional flow area that appear in the Reynolds number and heat transfer calculations. A square pitch produces a larger De and a more open flow path, lowering the mass velocity and the resulting shell‑side heat transfer coefficient (ho). A triangular pitch packs tubes tighter, creating a smaller De, higher velocity, and greater turbulence—yielding a higher ho but also a larger pressure drop.
In any pilot‑plant heat exchanger, the pitch geometry is the fundamental lever that sets the shell‑side hydraulic diameter and flow area. These two variables cascade through the Reynolds number and empirical Nusselt correlations to determine ho. The choice is a deliberate trade‑off: triangular pitch maximizes heat transfer at the cost of pressure drop and cleanability, while square pitch sacrifices some thermal performance for easier mechanical cleaning and lower flow resistance.
How Tube Pitch Alters the Shell‑Side Calculation
The shell‑side heat transfer coefficient emerges from a sequence of calculations that all begin with the tube layout geometry. Understanding this pathway reveals exactly where the pitch exerts its influence.
The Equivalent Diameter Changes First
The pitch geometry defines the shell‑side equivalent diameter (De). De is not a physical pipe dimension—it is a hydraulic parameter that converts the irregular flow cross‑section between tubes into an equivalent circular channel.
For a square pitch, the unit cell free‑flow area is Pt² – π·do²/4 and the wetted perimeter is π·do. After accounting for row effects in a tube bundle, the effective De becomes:
De_square = 4 × (Pt² – π·do²/4) / (12 × π·do)
For a triangular pitch, the effective De calculated from a similar unit cell but using the triangular flow area gives:
De_tri = [4 × (0.5·Pt × 0.86·Pt – 0.5 × π·do²/4)] / (6 × π·do)
Because the triangular layout reduces the open space between tubes, De_tri is smaller than De_square for the same tube diameter and pitch ratio. This difference alone propagates through every subsequent step.
The Reynolds Number Reacts to Velocity and De
The shell‑side Reynolds number (Res) is De × Gs / μ, where Gs is the mass velocity (mass flow per unit cross‑sectional area). The cross‑sectional area itself is a function of the tube layout: a triangular pitch yields a smaller net free‑flow area for a given shell diameter, which forces a higher mass velocity.
Thus, a triangular pitch delivers a double hit: a smaller De and a larger Gs. Both effects increase the Reynolds number, pushing the flow deeper into the turbulent regime. A square pitch, with its larger De and lower velocity, results in a lower Reynolds number for the same shell‑side mass flow.
The Nusselt Number Captures the Difference
Empirical correlations translate the Reynolds number into the Nusselt number (Nu). The standard form for cross‑flow over tube bundles is Nu = C · Re^m · Pr^(1/3), where the constants C and m depend on whether the tubes are in an inline (square) or staggered (triangular) pattern.
Typical lab‑scale correlations for tube banks with many rows show:
- Inline (square) layout:
Nu ≈ 0.33 · Re^0.6 · Pr^0.33 - Staggered (triangular) layout:
Nu ≈ 0.26 · Re^0.6 · Pr^0.33
The triangular arrangement, despite a slightly lower pre‑factor, produces a higher Nusselt number because of the significantly larger Reynolds number it creates. The heat transfer coefficient is then ho = Nu × k / De. Here, the smaller De of the triangular pitch again amplifies ho, because De appears in the denominator.
The Net Effect on ho
In practice, a triangular pitch can deliver a 10–25 % higher shell‑side heat transfer coefficient than a square pitch for identical flow rates and fluid properties. The exact gain depends on the pitch‑to‑diameter ratio, baffle spacing, and operating conditions. The formulas above give students the tools to quantify this difference directly on a pilot‑plant data acquisition system.
Understanding the Trade‑offs
Higher heat transfer is not the only consideration. The same geometric features that boost ho also create practical constraints that a pilot plant is ideally suited to demonstrate.
Pressure Drop Rises with Heat Transfer
A smaller De and higher velocity increase the friction factor. The shell‑side pressure drop scales with the square of velocity and inversely with De. The triangular pitch, which raises ho, inevitably leads to a larger pressure loss across the shell side. This trade‑off becomes visible when students compare pump power requirements between the two configurations under the same thermal duty.
Mechanical Cleaning Becomes Difficult or Impossible
A square pitch creates straight, unobstructed lanes between tube rows. With a minimum clearance of 6.4 mm (0.25 in), these lanes allow brushes or mechanical scrapers to pass through. A triangular pitch eliminates those continuous lanes, making mechanical cleaning of the shell side impractical. If the process fluid fouls heavily, a triangular layout will suffer rapid performance degradation that a pilot plant can measure over time.
Thermal Effectiveness vs. Maintainability
The choice is ultimately between maximizing the instantaneous heat transfer coefficient and preserving long‑term cleanability. In a pilot plant, students can operate both configurations with a fouling‑prone fluid and observe how the initially higher ho of the triangular layout decays, while the square layout maintains a more stable (though lower) coefficient because it can be cleaned between runs.
Making the Right Choice for Your Pilot Plant Goal
The geometry you select should align with the learning outcomes or experimental objectives of the exercise.
- If your primary focus is demonstrating maximum heat transfer efficiency: Choose a triangular pitch. It will produce the highest Reynolds numbers and the largest ho, allowing you to clearly show the impact of turbulence and flow velocity on thermal performance.
- If your primary focus is studying fouling, maintenance, or pressure‑drop trade‑offs: Select a square pitch. The accessible tube lanes make it possible to mechanically clean the shell side and to show the real‑world consequences of layout choice on operational costs.
- If your primary focus is a versatile, multi‑fluid teaching platform: Opt for a square pitch with the recommended 1.25‑times‑diameter pitch and a minimum 6.4 mm gap. This configuration safely handles a wider range of fluids, including those that foul, and still provides a clear, measurable ho difference for comparison with triangular data from literature.
The tube pitch geometry is not a minor design detail—it is the starting point for every shell‑side calculation, and the pilot plant makes that dependency tangible.
Summary Table:
| Feature / Parameter | Square Pitch | Triangular Pitch |
|---|---|---|
| Equivalent Diameter (De) | Larger | Smaller |
| Flow Velocity & Turbulence | Lower | Higher |
| Heat Transfer (ho) | Lower (Baseline) | Higher (10–25% gain) |
| Pressure Drop | Lower | Higher |
| Mechanical Cleaning | Easy (unobstructed lanes) | Difficult / Impractical |
Elevate Your Engineering Lab with LABPARK Pilot Plants
Hands-on experience with heat exchanger geometry is crucial for tomorrow's engineers. LABPARK designs and manufactures high-quality Educational and Vocational Unit Operations Pilot Plants for chemical engineering, bioprocess & biotech, and environmental & water treatment. We help universities, research institutes, and enterprises bridge the gap between theory and practice.
Ready to upgrade your laboratory? Contact us today to discuss your customized pilot plant needs!
Related Products
- Shell and Tube Heat Exchanger Heat Transfer Coefficient Determination Educational Pilot Plant
- Three-Tube Heat Transfer Educational Pilot Plant for Unit Operations Training
- Comprehensive Multi-Modal Heat Transfer Unit Operations Pilot Plant for Engineering Training
- Dual Mode Heat Transfer Pilot Plant for Unit Operations Training
People Also Ask
- Why Apply LMTD Correction in Shell-and-Tube Pilot Plants & How to Determine It
- How is the fouling factor (Rd) evaluated? Key Pilot Plant Insights for Students
- How is fouling factor demonstrated using shell and tube pilot plants? Practical Lab Guide
- Why is simulating and calculating fouling factors crucial when operating educational heat exchanger pilot plants?
- How do tube pitches affect equivalent shell diameter (De)? Math & pilot plant impact explained.